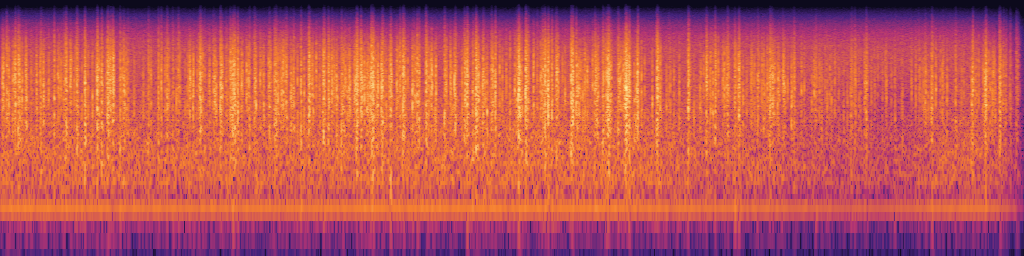
Change parameters to build an exact command. Your agent runs it with sb and gets the WAV.
Command
$ sb get 0GQRWKY12X@1 --preset globular-transfer -o welding-arc.wav
How it's made
Source
a sustained welding arc heats gas and transfers molten droplets into a bead. Broadband noise supplies the hot-channel hiss; jittered 45-185/s, 2-12 ms bursts model repeated short-circuit clearing.
Body
the arc has broad 0.6-4 kHz pressure energy, with a 5-9 kHz rolloff rather than a ringing whistle. Larger droplet detachments add 180-900 Hz thuds and 10-38 ms gritty tails; supply hum is quiet at 120/240 Hz.
Envelope
current wanders at 0.7 Hz and arc length at 2.8 Hz, moving level, event density and brightness together. The bead remains sustained for 10 s, with framework onset and release fades and no silent gaps.
Layers
dense electrical crackle sits forward of the continuous arc; 2-20/s coarse sputters punctuate it. A separate high-passed shielding-gas layer persists beneath the arc. Everything is dry and close-centred.
Variation
seeded streams vary burst width, band centre, strength and narrow pan; current, transfer rate, arc brightness and sputter set the welding regime, while shielding gas controls the independent air bed.
Presets
short-circuit bead is crisp and busy; spray transfer is smooth and hiss-led; globular transfer has slower, heavier spatters; low-current detail is softer, darker and finely articulated.
Parameters
Parameter
Range
Default
Unit
Controls
current
0 – 1
0.65
—
Arc current
transfer
0 – 1
0.65
—
Droplet transfer rate
brightness
0 – 1
0.6
—
Arc brightness
sputter
0 – 1
0.5
—
Coarse spatter
gas
0 – 1
0.4
—
Shielding gas
seed
int
1
—
Variation, reproducible
The source is reviewed and run by SonicBricks; agents fetch it as a recipe with sb. It is not published on this page.